Precision Automated Racks & Specialized Storage Systems
As a dedicated OEM/ODM manufacturing facility, we engineer, fabricate, and export high-performance automated warehousing substructures, automated bin retrieval matrices, and heavy-duty sheet storage solutions built to integrate natively with global Crane, Shuttle, and WCS controllers.
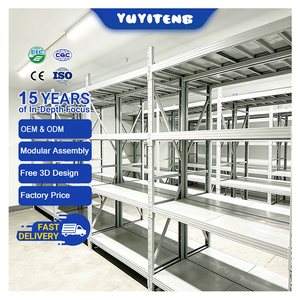
Storage Shelving Units Commercial Movable Shelving
High-density mobile aisle shelving mounted on gear-driven precision steel rails. Eliminates static access aisles to reclaim up to 85% of floor space in commercial and parts depots.
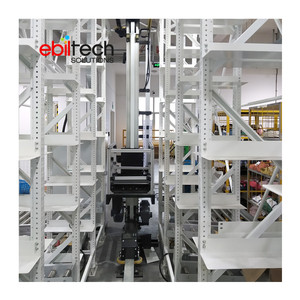
Automated Storage Miniload ASRS Storage System
High-bay miniload substructure engineered for ultra-lean tolerances and high horizontal/vertical stacker crane acceleration. Ideal for high-throughput automated carton buffering.
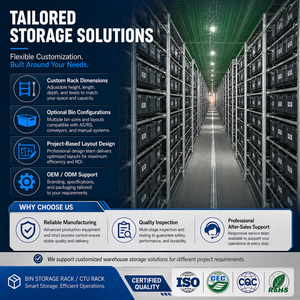
Mini Load ASRS Tote Storage Rack Bin System
Engineered for e-commerce, pharmaceutical, and electronic micro-fulfillment. Features roll-formed side guides, micro-pitch adjustability, and integrated picking chutes.
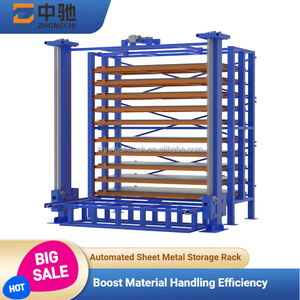
Intelligent Automated Steel Sheet Metal Storage Rack
8-layer heavy-duty structural steel cassette tower built for raw plate inventory. Direct interfacing with automated vacuum lifters, laser cutting loaders, and CNC sheet feed systems.
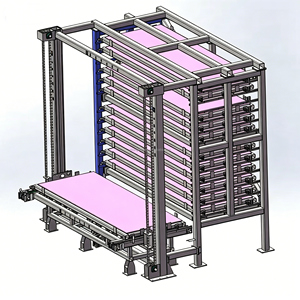
Electric Heavy Duty Sheet Metal Drawer System
Motorized or crank-out drawer racks providing 100% overhead crane accessibility to individual heavy metal sheets, heavy stamping molds, dies, and tooling fixtures.
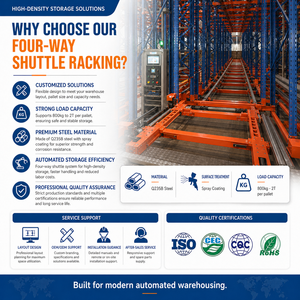
Automated Four-Way Shuttle Pallet Racking System
Extreme-density multi-directional pallet matrix. High-precision track sections allow autonomous 4-way shuttles to navigate cross-aisles and multi-level vertical lifts seamlessly.
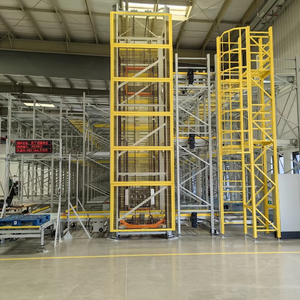
Selective Pallet Rack with Conveyor Integration
Heavy structural racking paired with continuous roller, chain, and transfer conveyors. Designed for automated dispatch staging, pallet flow buffers, and sortation hubs.
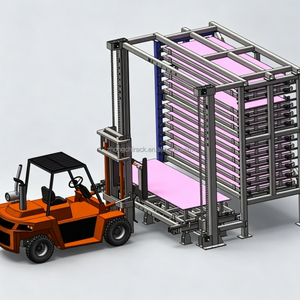
Vertical Sheet Storage Rack with Robot Loading
Fully enclosed automated vertical plate warehouse featuring robotic picking arm connectivity, dynamic thickness-gauging inventory logic, and real-time cassette shuttles.
Factory-Direct OEM/ODM Engineering: Why EPCs & Global Integrators Partner With Us
In high-bay automated warehouses, racking is not passive steel furniture; it is the structural skeleton of the entire robotic automation loop. Tolerances of fractions of a millimeter dictate whether an ASRS crane runs at 300 m/min or experiences catastrophic sensor trips.
Continuous CNC Roll-Forming
Our facility operates 28 multi-stage continuous roll-forming production lines equipped with in-line servo punching. Upright profiles achieve dimensional repeatability within ±0.5 mm over 18-meter single-piece columns, guaranteeing perfect crane rail alignment.
Finite Element Analysis (FEA)
Every bay profile undergoes rigorous structural FEA modeling according to EN 15512:2020 and RMI standards. We factor in second-order elastic-plastic analysis, dynamic crane acceleration loads, seismic base shears, and local buckling limit states.
Thermoset Anti-Corrosion Finishing
Automated pre-treatment, nano-ceramic zirconium cleaning, and dual-station electrostatic powder coating ensure paint adhesion that resists thermal shock from -30°C cold stores to +55°C hyper-arid desert distribution hubs across the Middle East, Africa, and Americas.
Turnkey Global Export Packaging
Custom structural steel bundling, seaworthy rust-inhibiting wrapping, color-coded bay sequencing, and component-tagged export packing ensure that automated substructures arrive with zero transit twist, ready for rapid on-site mechanical erection.
System Architectures: Load Mechanics, Clearances & Throughput Calculations
Procuring automated storage racks demands matching storage density with dynamic retrieval cycles. Below is our engineering benchmark across core automated racking structural typologies.
| System Architecture | Payload Class | Max Structural Height | Vertical Deflection Limit | Throughput Capacity | Primary Sector Fit |
|---|---|---|---|---|---|
| Unit-Load Crane ASRS | 500 - 2,500 kg / pallet | Up to 40 meters | L / 300 to L / 400 | 35 - 55 pallets/hr per crane | Bulk distribution, Cold chain, Chemical IBCs |
| Miniload Tote / Carton ASRS | 30 - 100 kg / bin | Up to 24 meters | L / 400 (strict tolerance) | 120 - 250 cycles/hr | Pharma, Electronics, Micro-fulfillment |
| 4-Way Radio Shuttle Matrix | 1,000 - 1,500 kg / pallet | Up to 22 meters | L / 250 | Flexible (Scalable via shuttle fleet) | High-density SKU consolidation, Beverage, 3PL |
| Heavy Sheet Metal Cassette Towers | 2,000 - 5,000 kg / drawer | Up to 12 meters | L / 500 (zero plate sagging) | 10 - 20 cassette cycles/hr | Laser cutting, Aerospace stamping, Heavy fabrication |
The Engineering Science Behind Structural Deflection in ASRS Racking
Unlike standard selective pallet racking designed primarily for static gravity loads governed by localized forklift operator judgement, an automated rack structure acts as a rigid kinematic machine guide. Beams, column base plates, and horizontal/vertical bracing channels must withstand continuous dynamic load oscillations induced by rapid deceleration of automated shuttles and cranes.
At our factory, our hot-rolled and cold-formed coil steels are sourced strictly under certified mill certifications (standard ASTM A1011 SS Grade 50 or European EN 10025 S355JR). Punching patterns are executed before roll forming to ensure structural grain continuity. Beam connectors feature 4 or 5 heavy-duty cold-forged locking pins that maximize joint rigidity ($C_d$ connection stiffness values), preventing frame sway even when rack heights exceed 30 meters.
Procurement Trends: How Intralogistics Buyers Are Sourcing Racks for 2025–2030
Macro supply chain volatility, land acquisition costs, and explosive robotic automation adoptions are reshaping what procurement managers look for in automated storage contracts.
Decoupled Fleet & Steel Procurement
Procurement directors are shifting away from monolithic proprietary automation vendors. Modern buyers procure open-standard steel substructures directly from OEM manufacturers like us, allowing them to freely choose shuttles, lifts, and software from independent robotics integrators at significant CapEx savings.
Transition from Cranes to 4-Way Shuttles
Fixed-aisle stacker cranes require dedicated aisle space for high-speed mast run-outs. Procurement data shows a 42% compound annual shift toward 4-way pallet shuttle matrix systems, which utilize 90% of warehouse cube volume and allow flexible addition of robots as throughput needs expand.
High-Tensile Thin-Walled Micro-Alloys
To reduce freight shipping costs and foundation slab structural loading, forward-thinking buyers specify advanced micro-alloy steels (e.g., Q355B and S420MC). By leveraging optimized profile moment-of-inertia cross-sections, overall rack tare weight is reduced by 14% while dynamic yield resistance increases.
Embedded Structural Health Sensors (SHM)
High-bay automated warehouses now incorporate IoT strain-gauge brackets and wireless 3-axis inclinometers at key base-plate anchors. Enterprise procurement frameworks now demand pre-machined mounting points on uprights for automated vibration and seismic displacement monitoring.
Sub-Zero Cryogenic Coating Technologies
With massive investments in pharmaceutical cold hubs and frozen food logistics, rack buyers are moving away from traditional wet paints. Demands have surged for special thermosetting powders that maintain high elasticity and zero embrittlement down to -35°C under continuous refrigeration cycles.
EPD Certified & Green Steel Documentation
Global supply chain tenders increasingly require Environmental Product Declarations (EPDs). Procuring through our state-of-the-art closed-loop powder-reclaim lines and energy-efficient roll forming allows overseas EPC contractors to meet stringent LEED and BREEAM industrial facility benchmarks.
Future Technological Advancements in Automated Storage Fabrication
The frontier of industrial automated storage is experiencing rapid technological convergence. Here is how our automated factory leads next-generation production processes.
1. Automated Robotic Welding & Fiber-Laser Cutting Arrays
Traditional manual welding introduces localized heat-affected zone (HAZ) variability and thermal warping. Our factory employs 6-axis robotic welding stations using digital pulsed synergic power sources. This guarantees full-penetration robotic welds on heavy-duty sheet metal drawer tracks, cantilever arm pivots, and crane anchor footplates, maintaining absolute dimensional fidelity across ten-thousand-component production batches.
2. Direct Native Integration with AMR / AGV Fleet Ecosystems
The boundary between static racks and dynamic robotics is dissolving. Our automated racks incorporate engineered precision pick-up and drop-off (P&D) stations, floor-docking alignment pins, and low-profile cantilever outriggers tailored specifically for Autonomous Mobile Robots (AMRs) and automated counterbalanced forklifts to dock without human guidance.
Key Manufacturing Milestones (2025 Roadmap)
- ✓ 0.1 mm Automated Optical In-Line Sorting: Real-time laser scanning on roll-forming lines to reject minor metal deviation instantaneously.
- ✓ Ultra-Tough Pre-Galvanized Post-Forming: Zero zinc-peel manufacturing for outdoor-facing automated vertical sheet storage units.
- ✓ Parametric Digital Twin CAD/CAM: Instantaneous generation of manufacturing toolpaths directly from client warehouse Revit / BIM files.
- ✓ Eco-Cure Low-Carbon Coatings: High-density cross-linked polymers curing at 160°C instead of 200°C, drastically lowering production carbon footprint.
Frequently Asked Questions for Automated Storage Rack Procurement
Clear, technically rigorous answers addressing critical engineering, tolerance compliance, international certification, and delivery logistics.
Partner with a World-Class Automated Racking Factory
Accelerate your warehouse automation schedule with reliable mill-direct capacity, precision automated roll forming, and certified structural safety assurance.