Featured Industrial Pipe Storage & Racking Systems
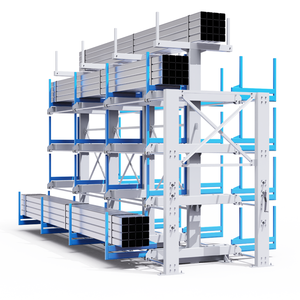
Explore our specialized range of structural cantilevers, adjustable long-goods shelving, and industrial pipe management systems engineered for heavy manufacturing, steel distribution, and logistics facilities.
Executive Whitepaper: Industrial Pipe Storage Architecture & Structural Integrity
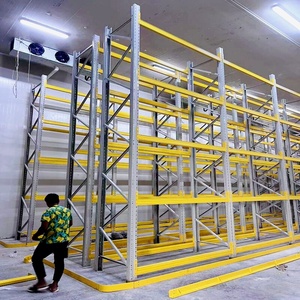
Managing long, heavy, and non-standard profile materials such as steel pipes, PVC tubing, copper conduits, and structural extrusions poses unique spatial and ergonomic challenges for industrial warehouse managers. Traditional pallet racking systems fail to accommodate the continuous linear dimensions of pipe stock, leading to sagging, high deflection rates, unsafe manual handling, and catastrophic floor space inefficiencies.
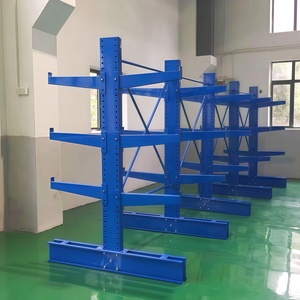
As a leading CE-certified pipe storage rack manufacturer and global exporter, our structural engineering team focuses on converting horizontal floor clutter into optimized vertical cubic storage. Utilizing heavy-duty hot-rolled Q235B and Q355B structural steel, our cantilever systems are engineered according to strict European structural standards (FEM 10.2.09 and EN 15512). This technical document outlines the mechanics, material choices, safety compliance, and future-proofing strategies necessary when procuring industrial pipe racking infrastructures.
FEA Load-Tested Arms
Every cantilever arm undergoes finite element analysis (FEA) to ensure zero permanent deformation under max rated capacity up to 6,000 kg per level.
CE Structural Compliance
Strict adherence to European Machinery Directive 2006/42/EC and EN 1090 structural steel execution standards, guaranteeing audit-ready safety.
Modular Pitch Adjustment
Vertical column punching at precise 100mm or 75mm increments allows effortless arm repositioning as inventory dimensions evolve.
Structural Steel Selection: Q235B vs. Q355B Hot-Rolled Columns
Selecting the appropriate steel grade is paramount to avoiding arm deflection and column buckling under asymmetrical pipe loading conditions. The table below details the structural metrics utilized in our manufacturing process:
| Parameter / Specification | Q235B Structural Steel | Q355B High-Strength Alloy | Impact on Pipe Racking Performance |
|---|---|---|---|
| Yield Strength ($f_y$) | 235 MPa | 355 MPa | Q355B increases arm load capacity by 51% without adding bulk weight. |
| Tensile Strength ($f_u$) | 370–500 MPa | 470–630 MPa | Provides superior resistance against sudden dynamic impact loads from forklifts. |
| Recommended Height | Up to 6.0 Meters | Up to 12.0+ Meters | High-bay automatic pipe storage requires Q355B structural columns. |
| Deflection Limit Ratio | $L / 200$ under full load | $L / 250$ under full load | Ensures tight tolerances for telescopic and crank-operated extension racks. |
Future Sourcing & Procurement Trends in Long-Goods Logistics
The industrial material handling market is undergoing a rapid transition toward high-density automation, ergonomic material retrieval, and sustainable manufacturing practices. Buyers and procurement heads must consider three core structural shifts over the next decade:
1. Transition to Telescopic & Roll-Out Cantilever Systems
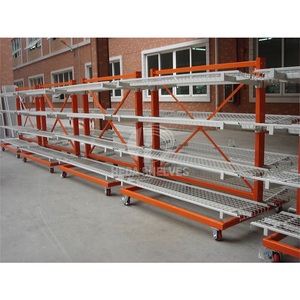
Traditional static cantilever racks require wide handling aisles (often 4.5 to 5.5 meters) to allow forklifts to maneuver long steel pipes horizontally. Procurement trends show a massive shift toward crank-operated and motorized telescopic cantilever racks. By allowing 100% full extension of the storage drawers, overhead cranes can access pipe stock directly. This reduces aisle space requirements by up to 65% and drastically minimizes forklift collision risks.
2. Integration of AS/RS with Stacker Cranes for Pipe Bundles
Automated Storage and Retrieval Systems (AS/RS) are no longer reserved solely for standardized wooden pallets. Modern heavy industry facilities are specifying specialized pipe cassette AS/RS solutions. These systems utilize automated honey-comb racks where pipe bundles are loaded into steel cassettes and retrieved via computer-controlled stacker cranes within seconds, integrating directly with ERP and WMS platforms.
3. RoHS & REACH Compliant Eco-Coatings
Environmental standards in international trade now mandate strict volatile organic compound (VOC) limits. Advanced powder-coating techniques utilize electrostatic polyester powder finishes cured at 200°C. This provides a salt-spray resistance exceeding 500 hours (ASTM B117 standard) while remaining completely free of heavy metals and hazardous solvents.
Industry & Product Development Trends: Next-Gen Pipe Racks
Safety engineering, IoT structural monitoring, and custom modularity represent the vanguard of storage rack evolution:
Smart IoT Load Sensors
Integration of strain gauges directly into column bases to alert facility managers of real-time structural overload or seismic shifts.
Pivot-Arm Safety Pin Systems
Arm connection joints engineered to pivot upwards and sideways upon impact from handling equipment, preventing catastrophic column damage.
Guided Rail Narrow Aisle (VNA)
Floor-mounted mechanical or magnetic guide rails integrated with side-loader forklifts allow aisle width reduction down to 2.1 meters.
Why Partner With Our Manufacturing & Export Infrastructure
As a global OEM/ODM manufacturer specializing in custom warehouse racking systems, our enterprise delivers structural engineering rigors that protect your workforce and optimize your bottom line:
1. Load-Engineered Precision: We do not rely on generic structural templates. Every proposal includes detailed CAD elevation drawings, floor slab load-distribution calculations, and certified beam connection schedules validated by licensed structural engineers.
2. Advanced CNC Manufacturing: Our automated production line features multi-head CNC punching machines, robotic seam welding stations, and automated roll-forming lines capable of processing profiles up to 12 meters in length with millimeter accuracy.
3. Comprehensive CE & International Certification: Our manufacturing plants operate strictly under ISO 9001:2015 Quality Management Systems. Every exported rack system carries a formal CE Declaration of Conformity, complying fully with EN 1090-1 and EN 15512 safety codes.
4. Global Logistics & Export Packaging: Export shipments are bundled using high-density steel strapping, protective corner guards, and heavy-duty moisture-barrier wrapping to guarantee zero surface abrasion or corrosion during transit across the UAE, Middle East, Europe, and Americas.
Frequently Asked Questions (FAQ) for Pipe Storage Procurement
Ready to Engineer Your High-Density Storage Layout?
Contact our engineering desk today for a complimentary CAD floor plan layout, static load calculations, and OEM factory-direct pricing.
Send an Inquiry